Featured Orthopedic Systems & Powered Bone Instruments
System-matched power saws, sternum resection units, modular limb kits, and anatomical simulation devices manufactured to exacting international clinical tolerances.
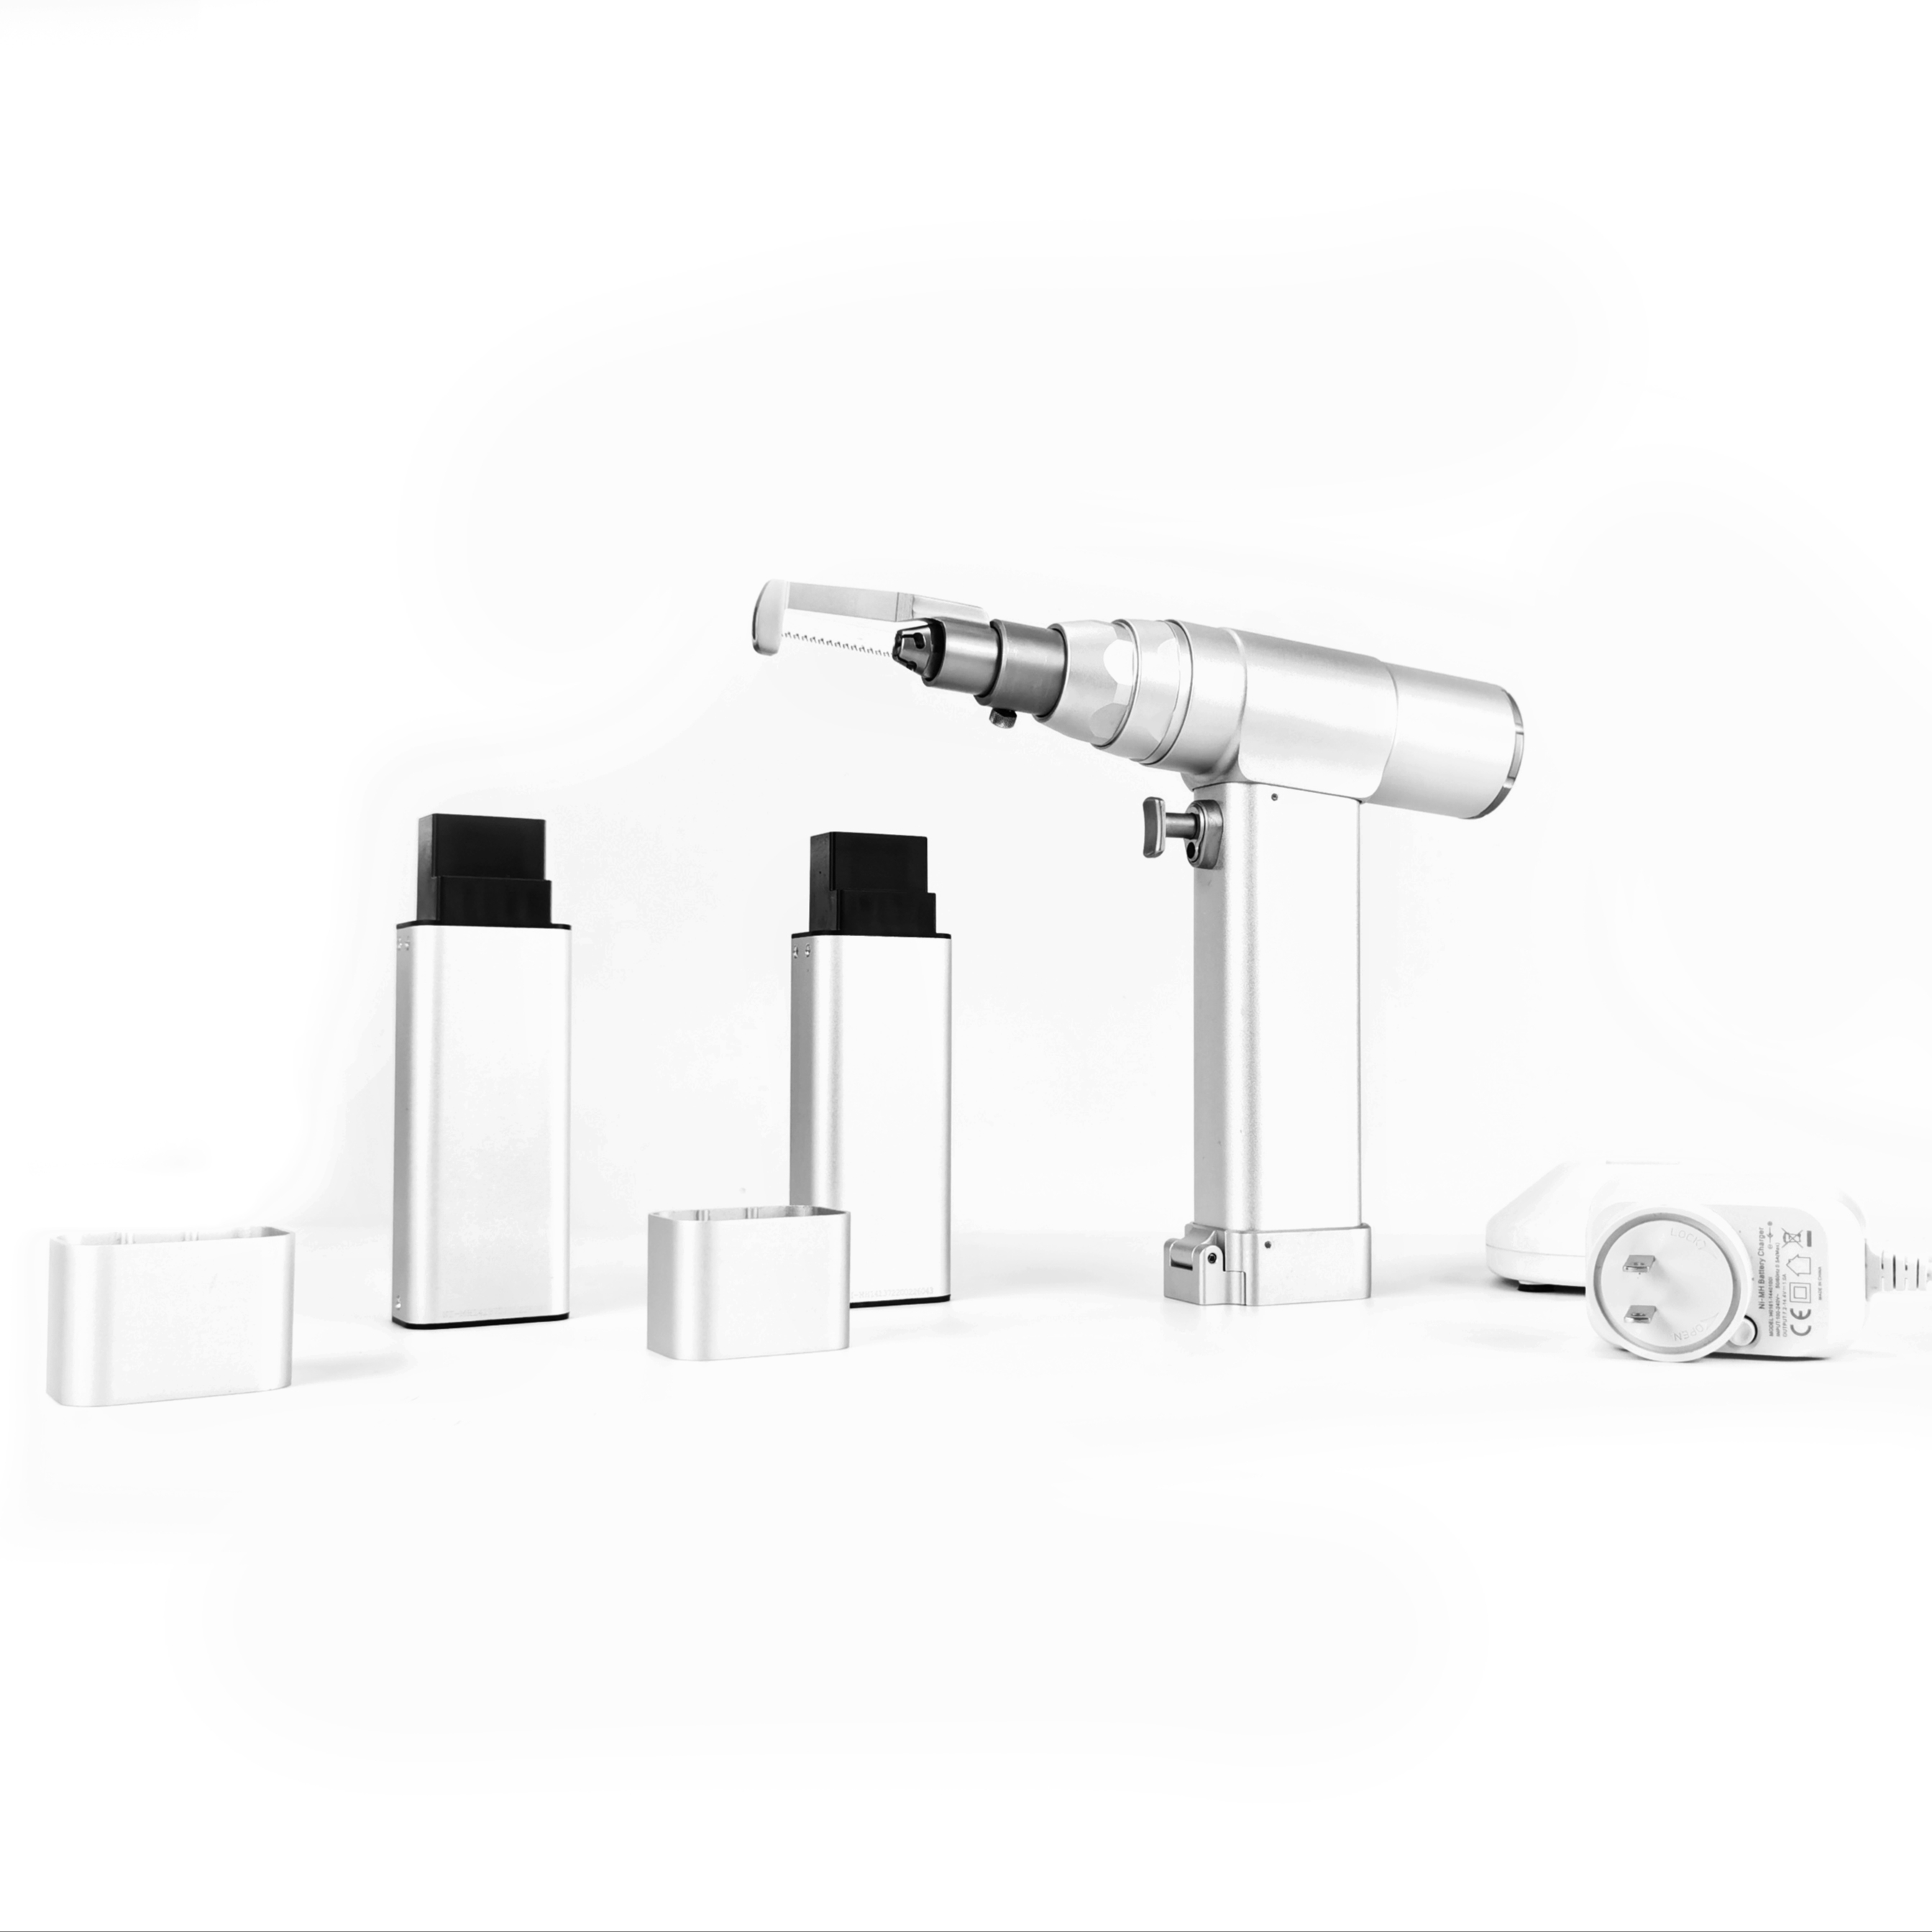
Factory Price Metal Sternum Saw Medical Electric Saw Orthopedic Drill Saw CE Certified
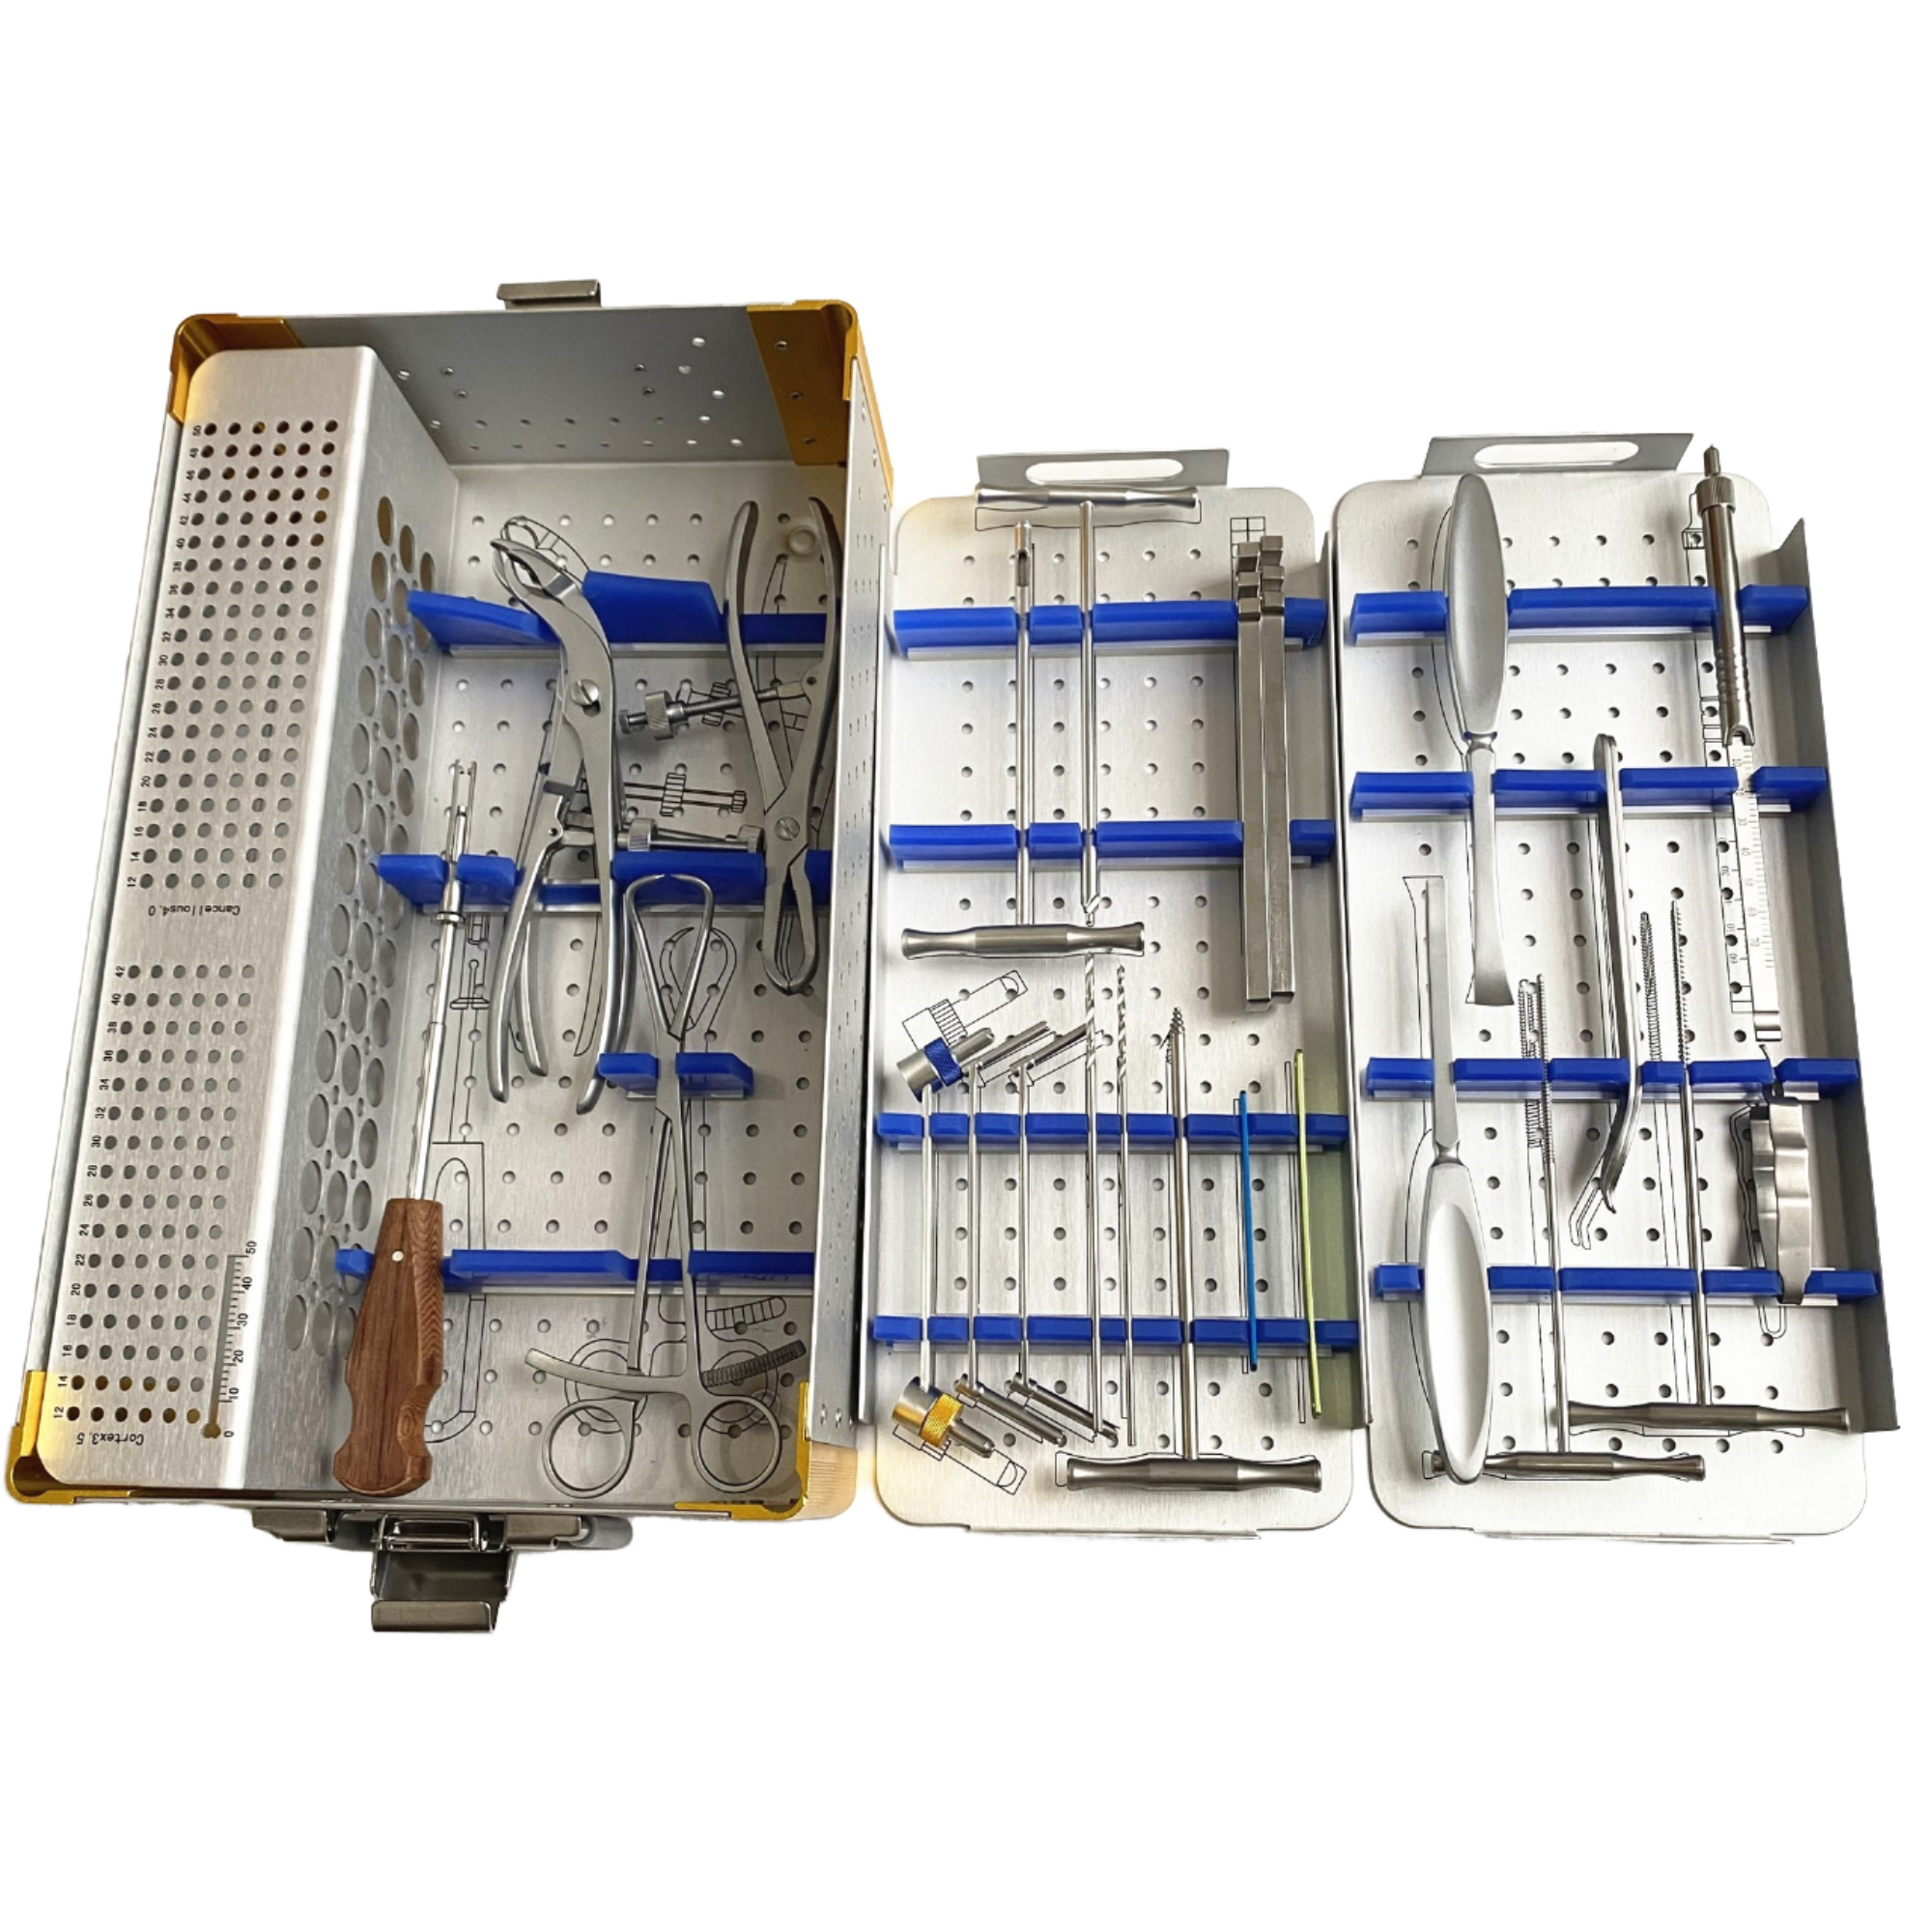
Small Fragment Orthopedic Upper Limb Instrument Kit Steel Bone Instruments

Orthopedic Instruments External Fixator Ringent Rod Coupling Clamp System
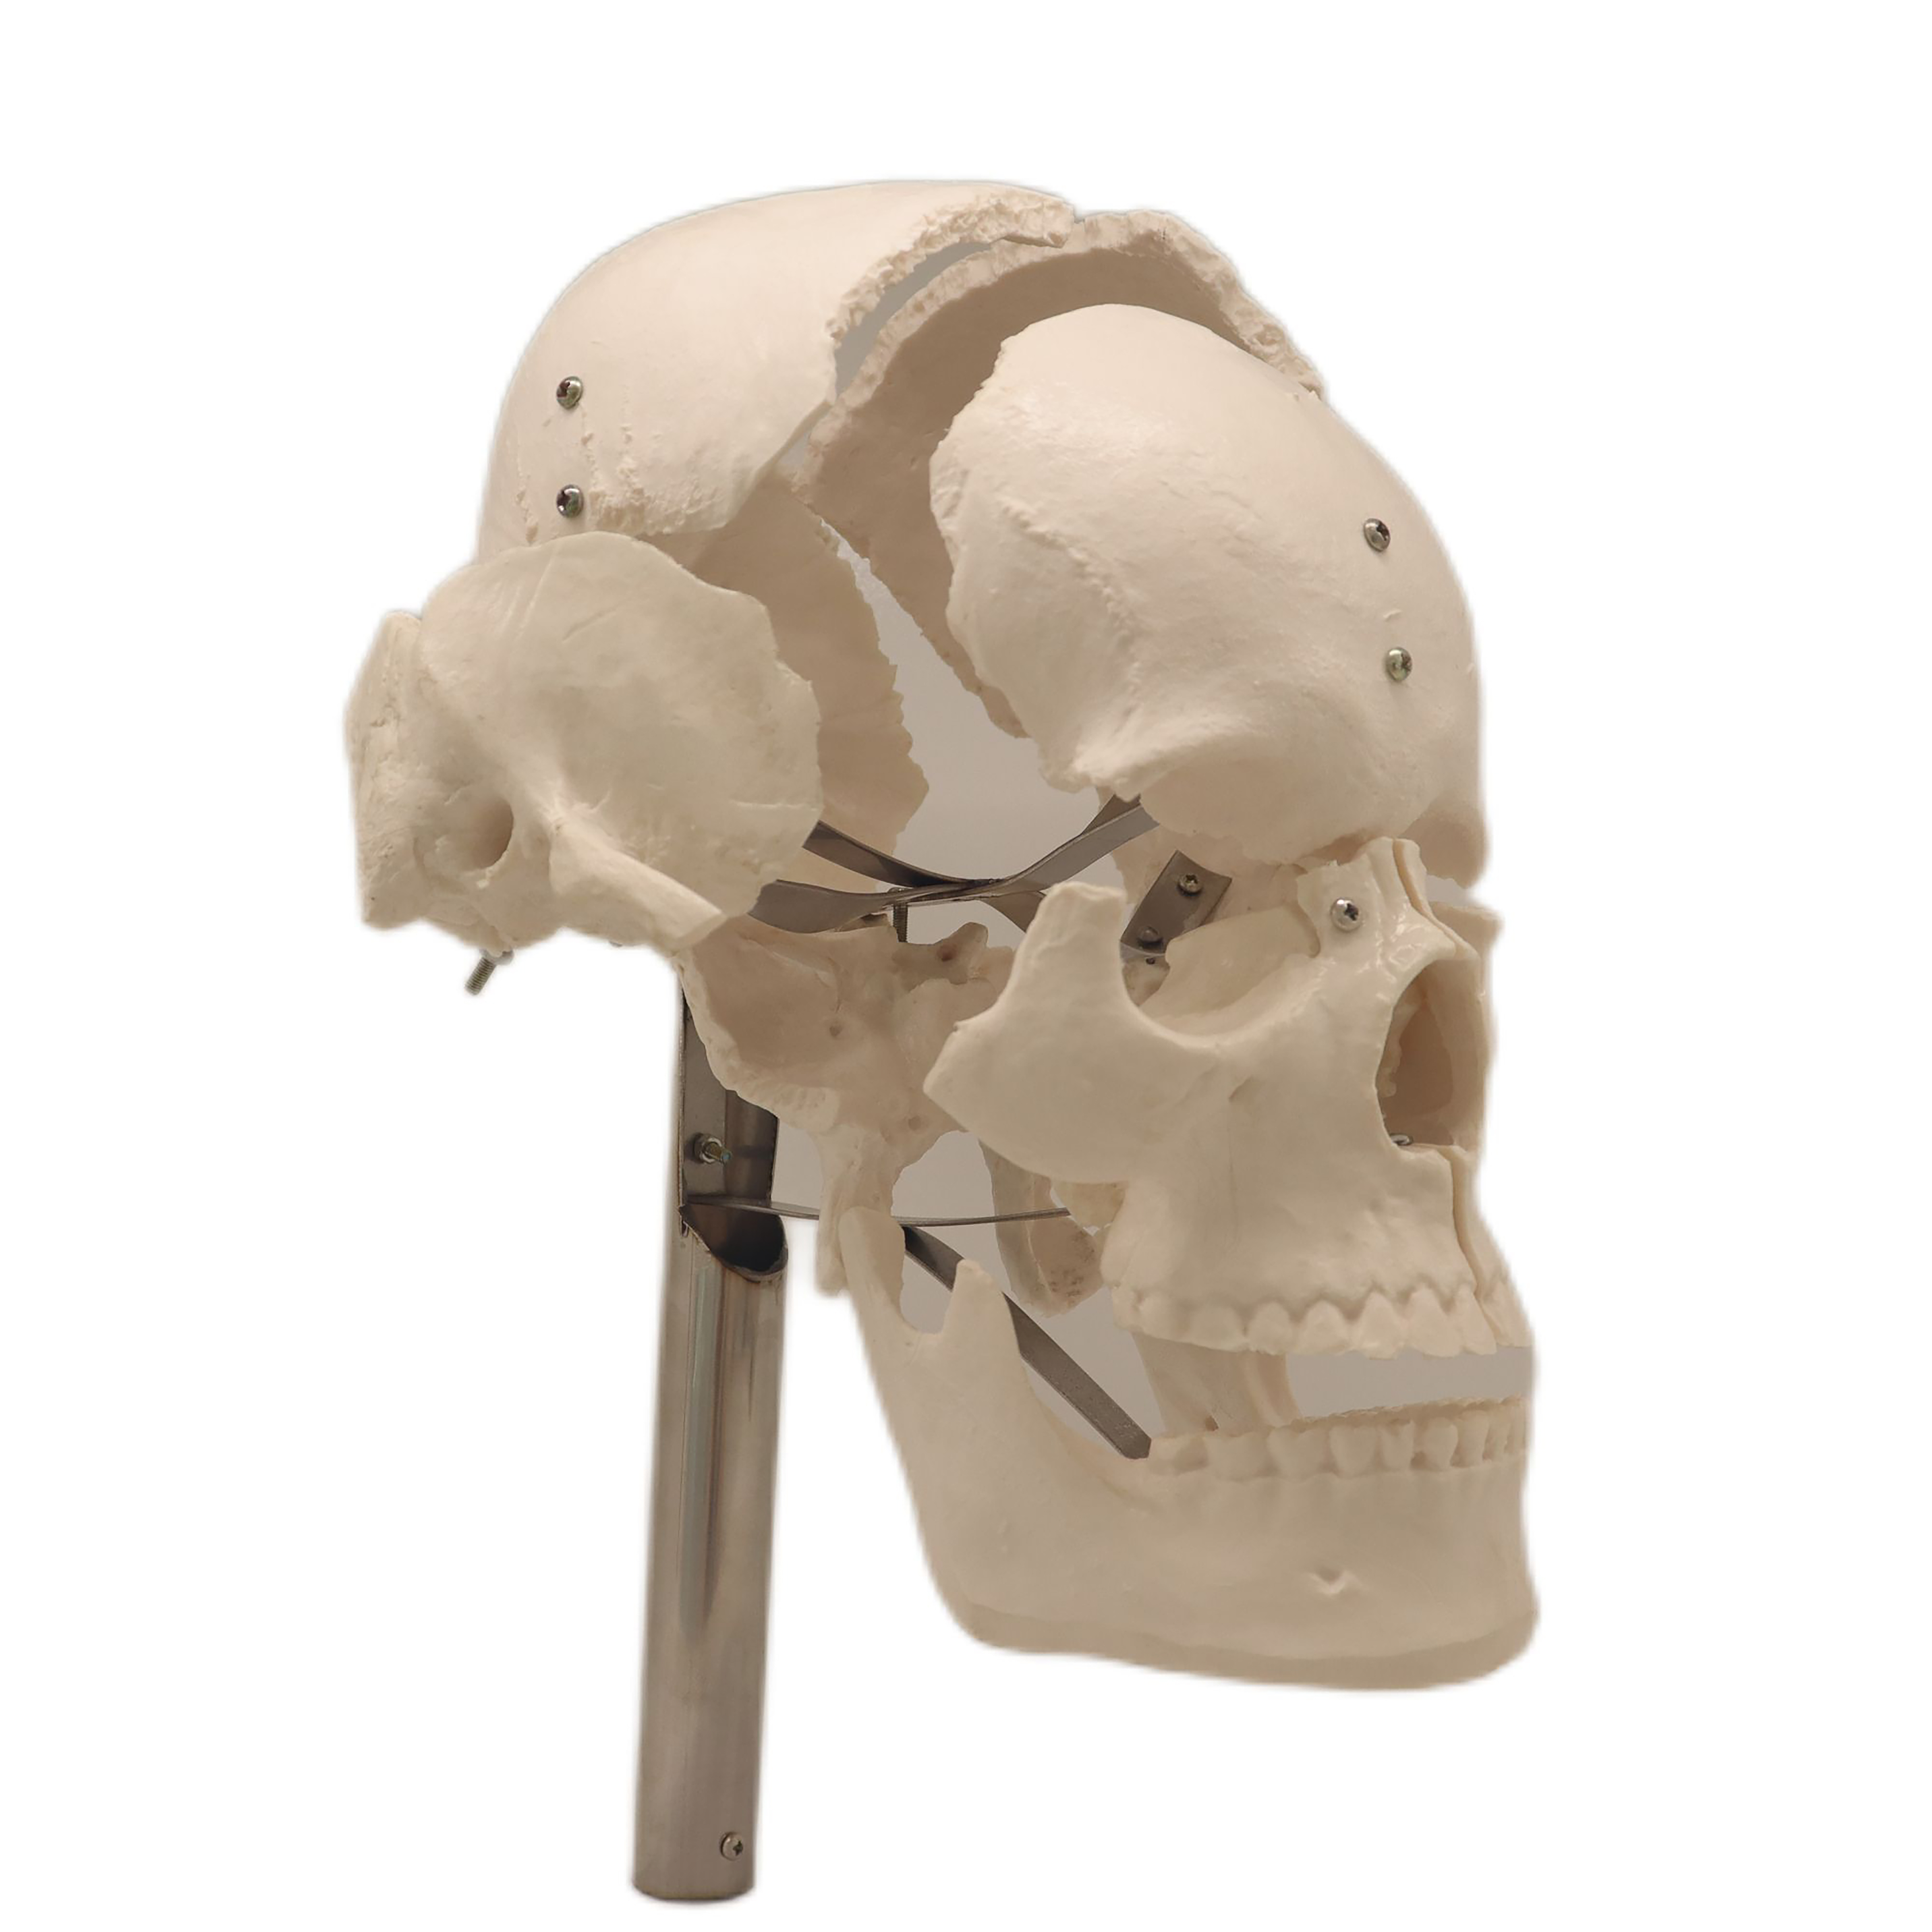
Lab Teaching Models: Separated Anatomical Human Skull Model in High-Grade PVC
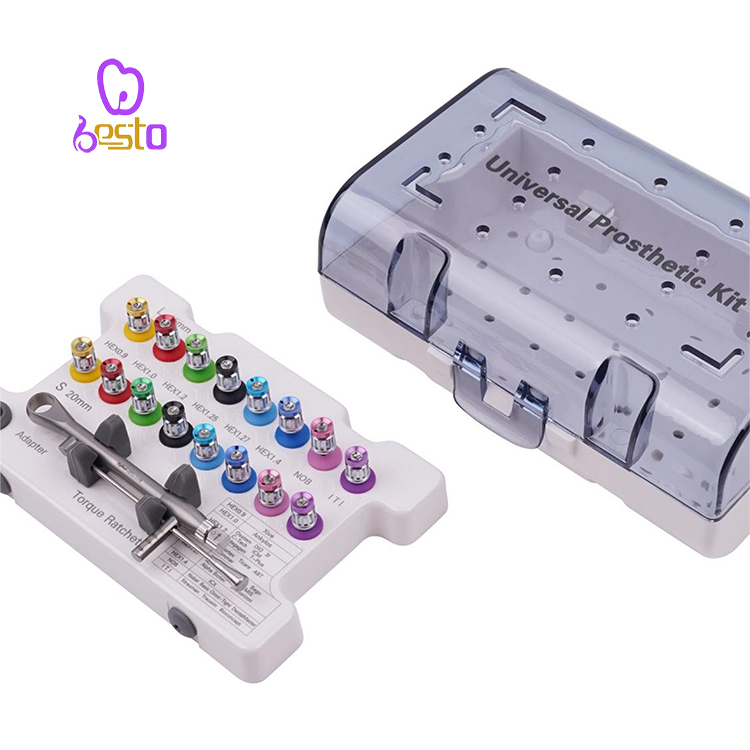
Electric Surgical Dental Implant Tool Box Steel Construction Handpiece System
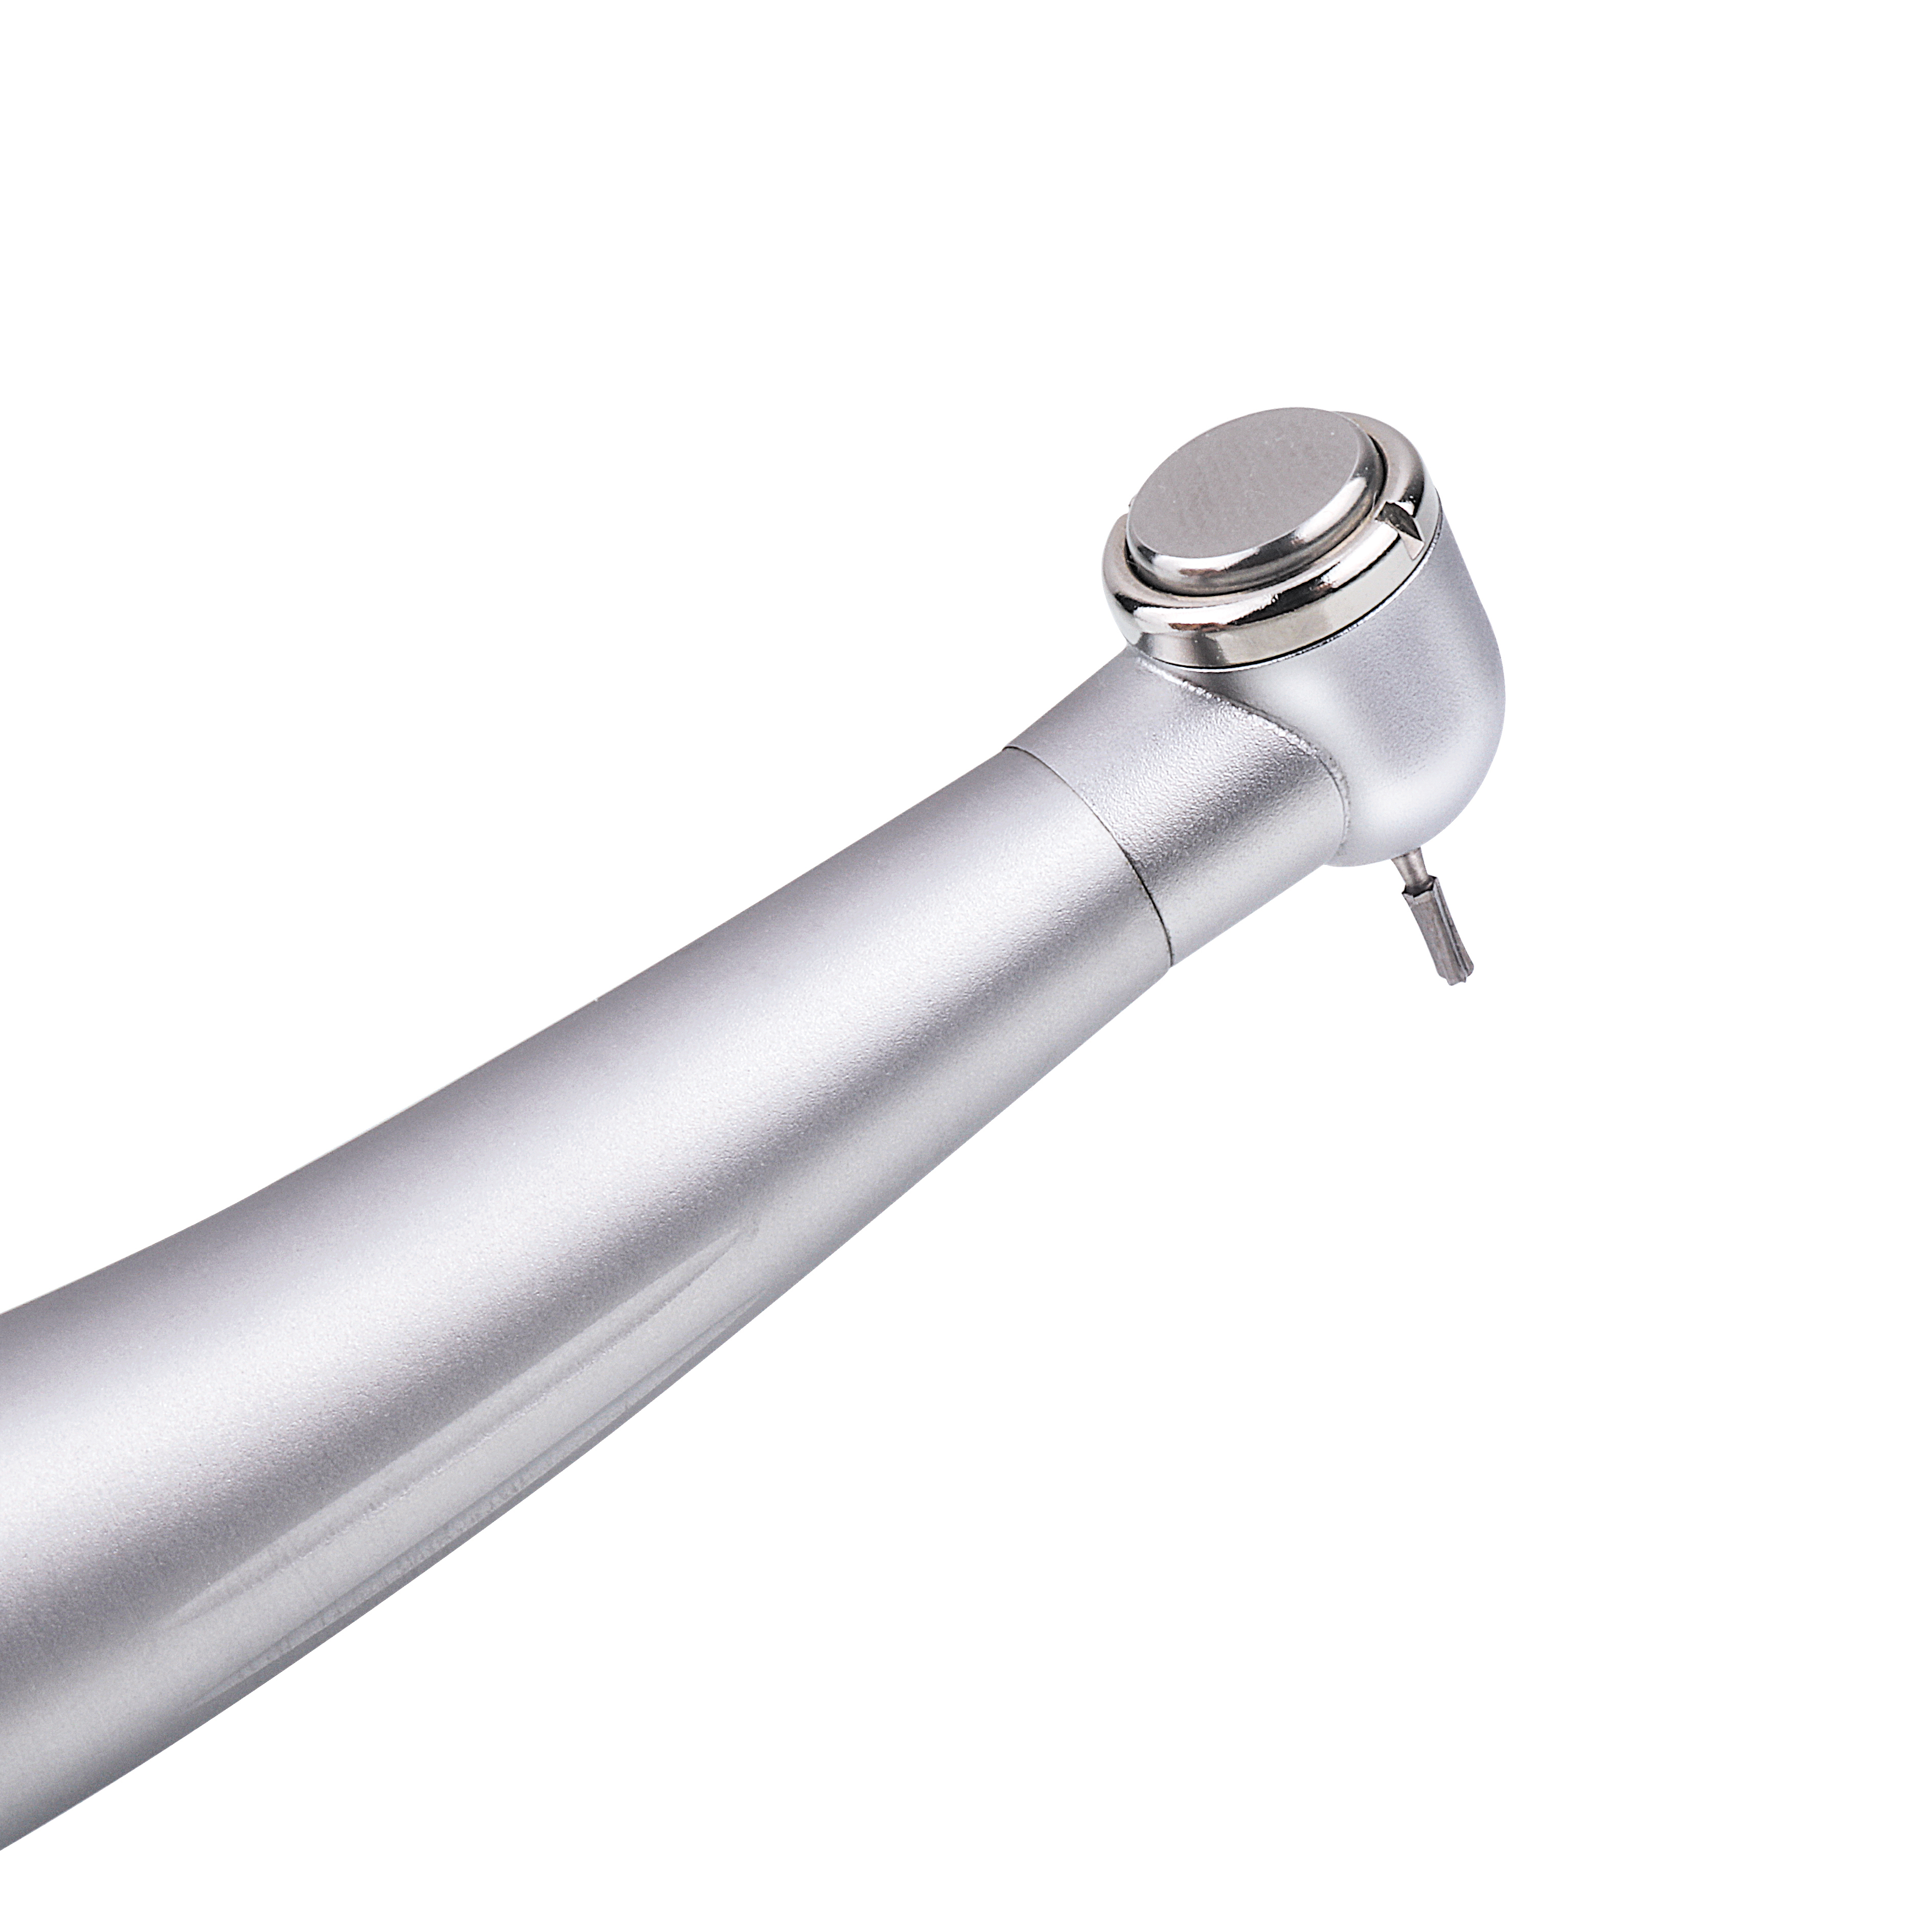
High-Speed Surgical Repair Handpiece for Dental Implants & Micro-Osteotomies
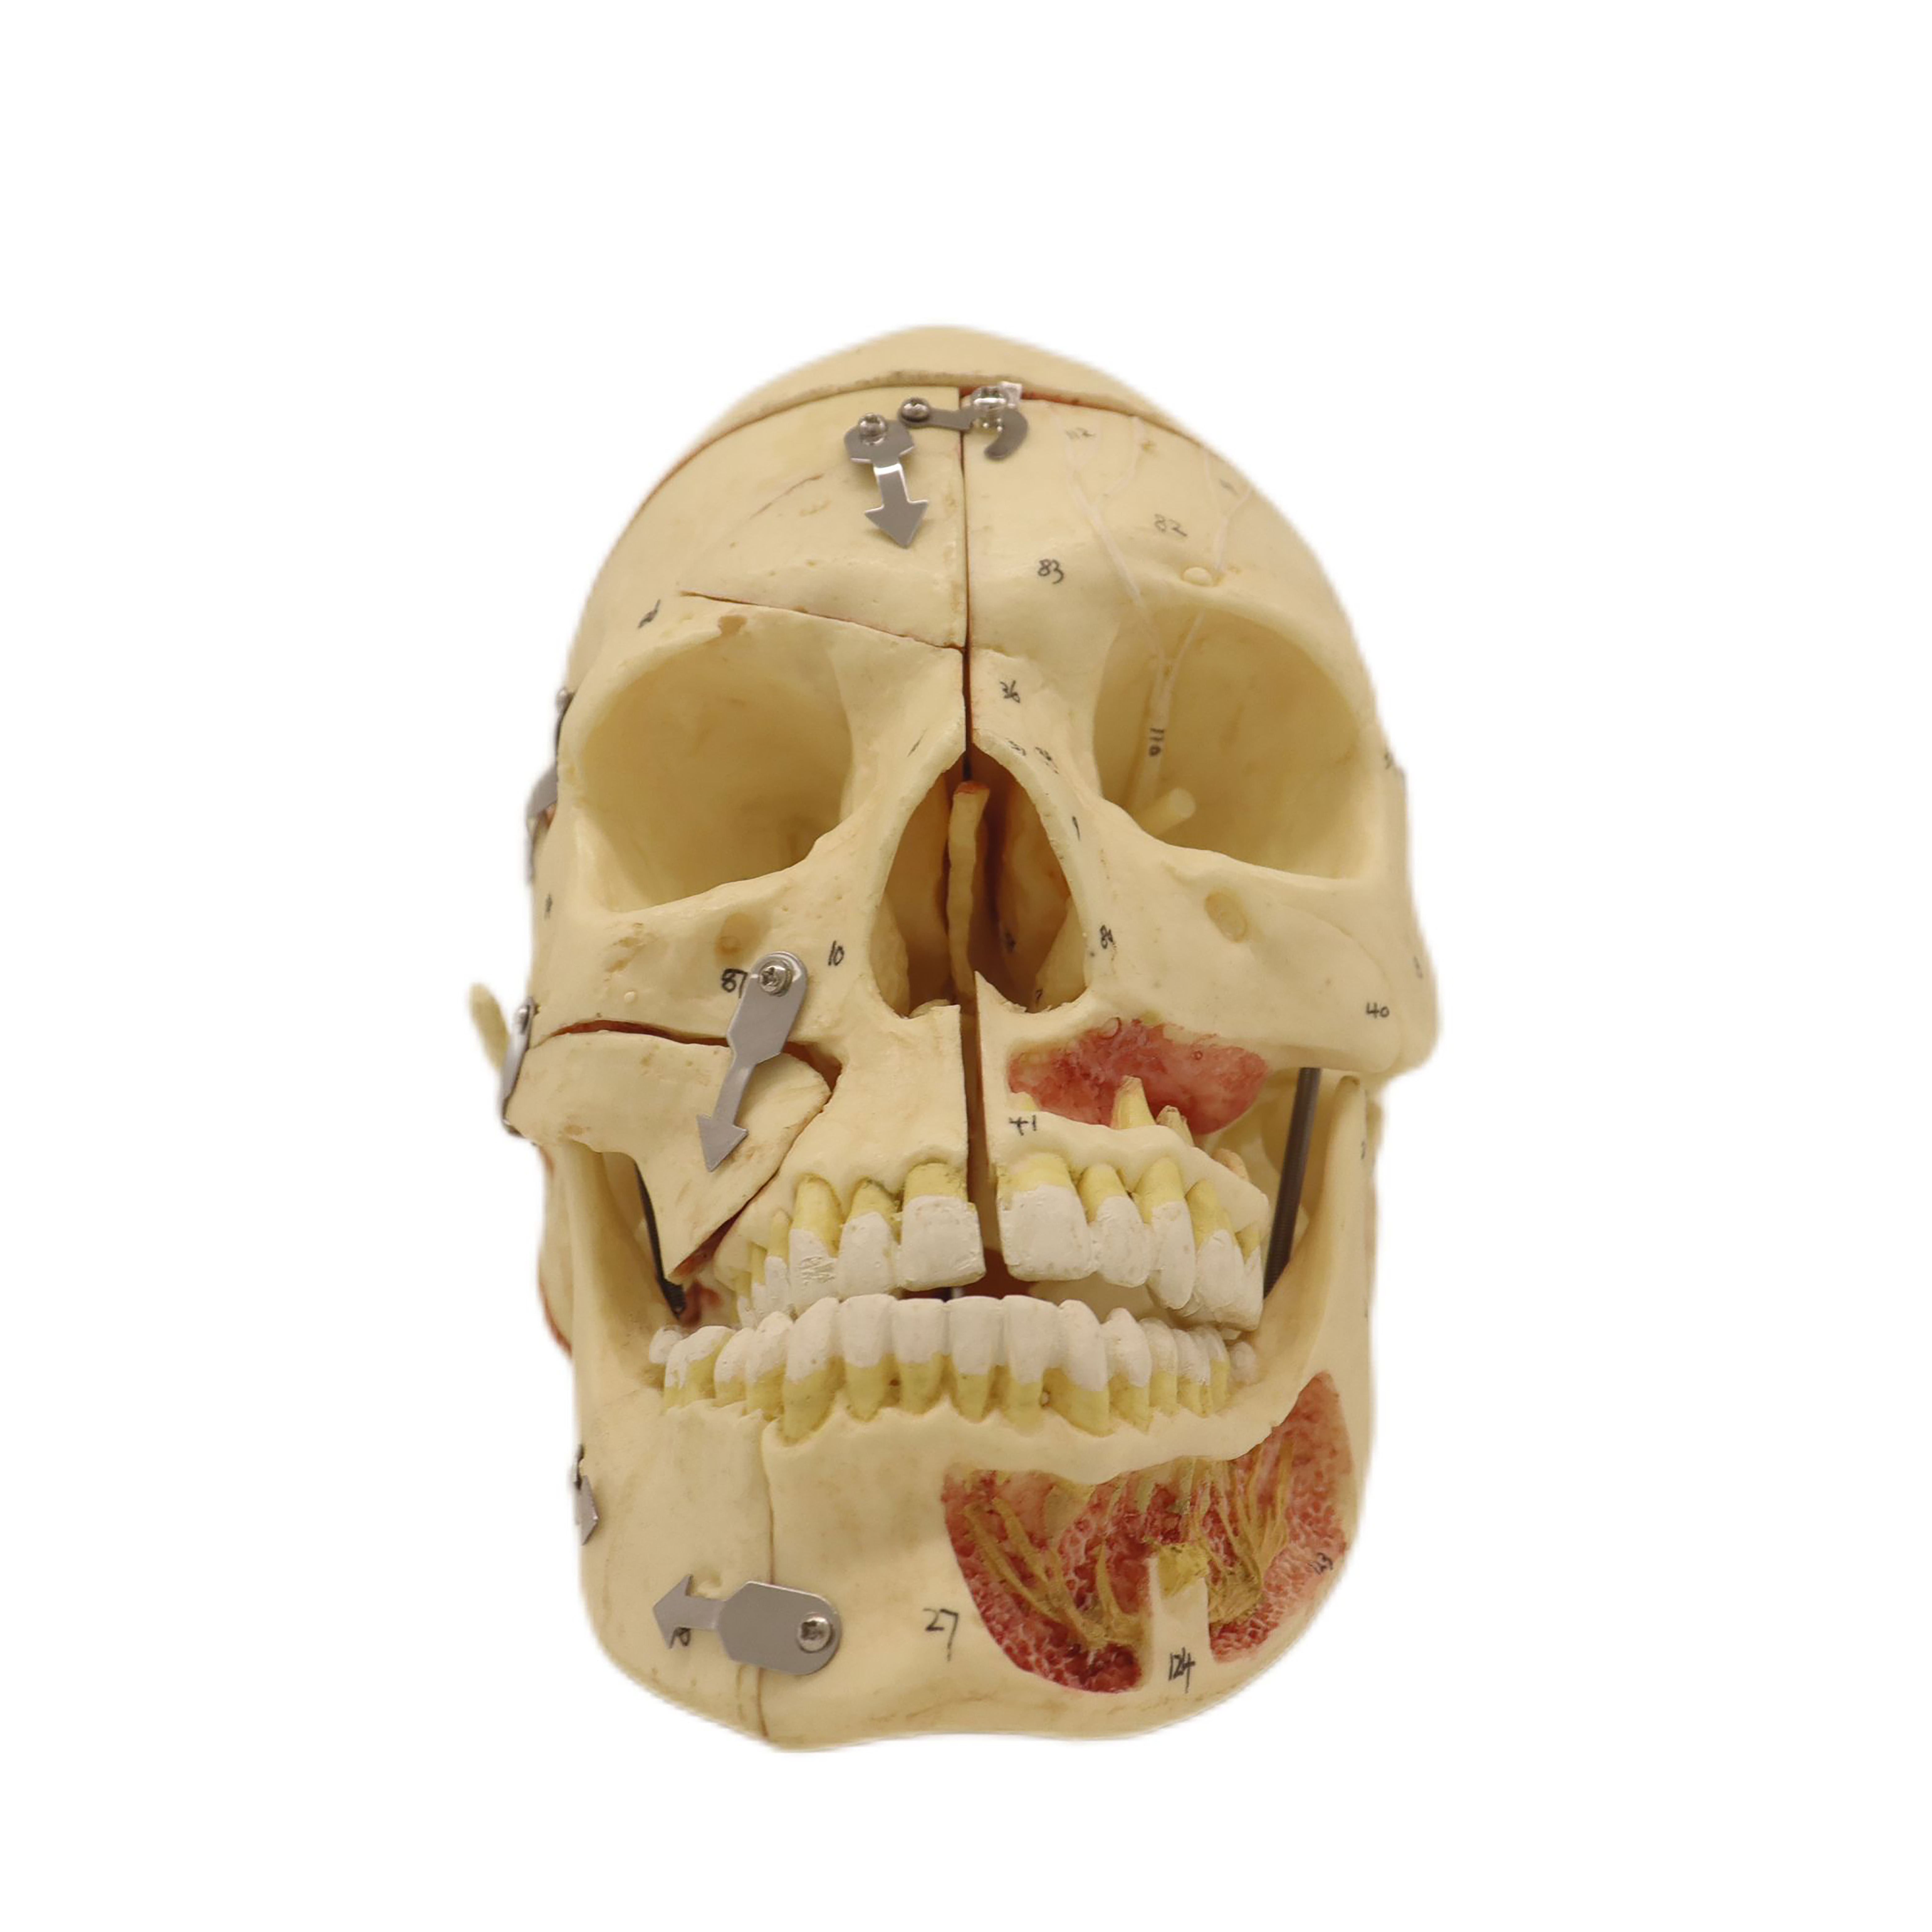
Lab Teaching Models: 3-Part Muscular Skull Skeleton Models for Academic Labs
Heavy Trauma Sagittal Bone Saw & Cannulated Orthopedic Power Drill System
Engineering High-Precision Surgical Saws for Modern Operating Theatres
A comprehensive treatise on dynamic cutting harmonics, osteonecrosis mitigation, micro-motor brushless architecture, and mechanical fatigue endurance.
1. The Biomechanical Imperative: Eliminating Thermal Necrosis in Cortical Bone
In joint arthroplasty, trauma osteotomy, and cardiothoracic sternotomy, bone resection is not merely a mechanical reduction task; it is a critical biological intervention. Cortical bone exhibits low thermal conductivity (approx. 0.38 to 0.52 W/m·K). Clinical histological research consistently demonstrates that when intraosseous cutting temperatures exceed 47°C for more than 60 seconds, alkaline phosphatase denaturation occurs, irreversibly destroying osteocytes and delaying the establishment of stable secondary osteons. As an OEM/ODM surgical saw manufacturer supplying premier European healthcare destinations such as Utrecht, Jiangsu GMV Medical designs reciprocating, sagittal, and oscillating drive assemblies that actively manage thermal generation at the micro-interface.
Our sagittal cutting blades utilize medical-grade martensitic stainless steel (grade 420 Mod / 440A) with precision diamond-ground rake angles (between 12° and 15°) and staggered offset kerf geometry. This specific kerf relief geometry facilitates rapid microscopic chip clearance, preventing bone slurry compaction along the lateral surfaces of the blade. In tandem with our optimized oscillating stroke frequency—calibrated between 12,000 and 15,500 oscillations per minute (OPM) through an angular excursion arc of 4.5° to 5.2°—frictional shear stress is minimized. This ensures that cutting temperatures remain well beneath the necrosis threshold, even during high-density cortical resections of the femur, tibia, or sternum.
“Thermal osteonecrosis at the resection plane is a primary, often under-diagnosed cause of early aseptic implant loosening. Managing cutting interface friction via engineered blade rake angles and calibrated harmonic excursion is the benchmark of high-tier surgical power tool manufacturing.”
2. Brushless DC Motor Architecture, Torque Stability, and In-Hand Balance
Conventional mechanical surgical tools historically relied upon brushed permanent magnet motors or pneumatic air turbine impellers. While pneumatic solutions offered compact power, they introduced significant logistical vulnerabilities: umbilical air hose encumbrance, potential lubricating oil mist deposition within laminar-flow clean air zones, and dependence on centralized medical gas infrastructure. Jiangsu GMV Medical has transformed surgical saw drivetrains by implementing proprietary Brushless DC (BLDC) motor platforms equipped with high-coercivity Neodymium-Iron-Boron (NdFeB) grade N45SH rotor magnets.
These brushless architectures eliminate carbon brush wear particulate and mechanical friction loss, translating to an ultra-efficient electrical-to-mechanical conversion efficiency surpassing 88%. More crucially for precision orthopedic and cardiothoracic surgeons, our closed-loop Hall-sensor digital motor control algorithms deliver uniform cutting torque (rated output ≥ 0.48 N·m) under dynamic mechanical loading. When the saw blade encounters dense cortical bone margins after traversing softer cancellous architecture, the micro-controller instantly modulates phase currents to prevent rotational stall or deflection without requiring excessive surgeon axial hand pressure.
Hermetic Autoclave Sealing
Double-encapsulated PEEK and medical-grade fluoroelastomer dynamic seals enable repeated 134°C prevacuum steam sterilization cycles conforming to EN 285 standards without casing moisture ingress.
Ergonomic Center-of-Mass
Engineered with a forward-tilted 115° handgrip angle and balanced lower-chassis battery housing, lowering surgeon pronator muscle fatigue index during prolonged reconstructive surgeries.
Universal Quick-Coupling Chuck
Toolless dual-cam locking collar accommodates international standardized sagittal blades, sternum guards, and K-wire attachments, ensuring smooth cross-compatibility in multi-vendor suites.
Surgical Saw Applications in Utrecht’s Premier Clinical Landscape
Meeting the operational criteria of university hospitals, high-volume cardiac institutes, and regional orthopedics across the Utrecht health corridor.
Emerging Clinical & Procurement Trends in Utrecht & the Benelux
How stringent EU Medical Device Regulations, sustainability initiatives, and centralized tender networks are reshaping medical device sourcing.
EU MDR 2017/745 Stringency
Dutch Notified Bodies and the Health and Youth Care Inspectorate (IGJ) impose zero-tolerance standards for device technical files, clinical evaluations, and post-market surveillance (PMS). GMV Medical provides complete technical dossiers, biocompatibility test records (ISO 10993), and risk matrices (ISO 14971) to ensure unhindered EU compliance.
The "Green OR" & Circular Healthcare
Dutch hospital purchasing consortiums (e.g., IntraKoop, Santeon network) are transitioning away from single-use disposable handpieces in favor of long-lifespan, repairable, energy-efficient powered surgical systems. Our modular drive units are built with field-replaceable mechanical gearboxes and environmentally inert lithium-iron phosphate battery chemistries.
Direct OEM Customization for European Brands
European orthopedic brands seek OEM manufacturing partners capable of white-labeling, custom laser etching with Dutch language markings, and system-matched sterile packaging. GMV Medical acts as an engineering extension, manufacturing custom handpiece geometries, unique blade chuck interfaces, and bespoke sterilization containment trays.
| Performance Characteristic | GMV Electric Brushless Saw | Standard Pneumatic Saws | Conventional Brushed Electric Saws |
|---|---|---|---|
| Motor Efficiency & Heat Dissipation | >88% Efficiency / Cold-Body Operation | Variable / Requires High CFM Flow | ~62% Efficiency / Significant Tool Warming |
| Autoclave Durability (134°C EN 285) | >800 Validated Sterilization Cycles | Sensitive to Air Line Moisture Condensate | Brush Degradation at ~250 Cycles |
| Acoustic Decibel Output | 61 – 65 dB(A) (Quiet Suite Compliant) | 74 – 82 dB(A) (Exhaust Air Hiss) | 70 – 76 dB(A) (Mechanical Resonance) |
| Rotational Stall Resistance | Real-Time Current Sensing Loop Control | Drops RPM Instantly Under Heavy Bone Load | High Rotor Inrush & Heating Risk |
| Operating Theater Mobility | Total Wireless Freedom (Li-ion Sealed Pack) | Restricted by 3m Pressurized Air Hose | Tethered Transformer or Heavy Pack |
| Biocompatible Housing Material | Aviation Al-Alloy + Hard Anodized Coating | Cast Nickel Plated Brass / Heavy Alloy | Polymer / Standard Anodized Alloy |
Why Utrecht Distributors and Hospital Groups Partner with Jiangsu GMV
Decades of proprietary machining expertise, verified by independent third-party assessors, controlling quality from raw medical alloy bar stock to sterilized surgical suite delivery.
TÜV Rheinland On-Site Verified
Our production facilities, testing laboratories, cleanrooms, and quality assurance processes have been inspected on-site by TÜV Rheinland, validating our engineering standards against strict international benchmarks.
In-House Multi-Axis CNC Machining
Equipped with high-precision CNC Swiss-type automatic lathes, 5-axis vertical machining centers, and automated wire EDM slitting equipment, maintaining dimensional tolerances within ±0.005mm.
Rigorous In-House Mechanical Testing
Every production batch undergoes optical projector dimensional verification, Rockwell/Vickers hardness testing, dynamic blade fatigue testing, and high-frequency torque curve verification in our QA labs.
Full-Spectrum OEM / ODM Engineering
We transform your hand-sketches, CAD drawings, or clinical prototypes into CE-ready orthopedic implants, specialized saw blades, sternal retractors, and powered handpieces under your private label.
Permanent Laser Traceability
Fiber laser marking machines encode batch numbers, GTIN barcodes, and unique device identification (UDI) directly onto titanium and stainless components for end-to-end hospital supply chain compliance.
Multilingual International Trade Team
Our export trade division supports European partners across customs clearance, Rotterdam/Schiphol freight routing, technical dossier transfers, and expedited sample prototyping.
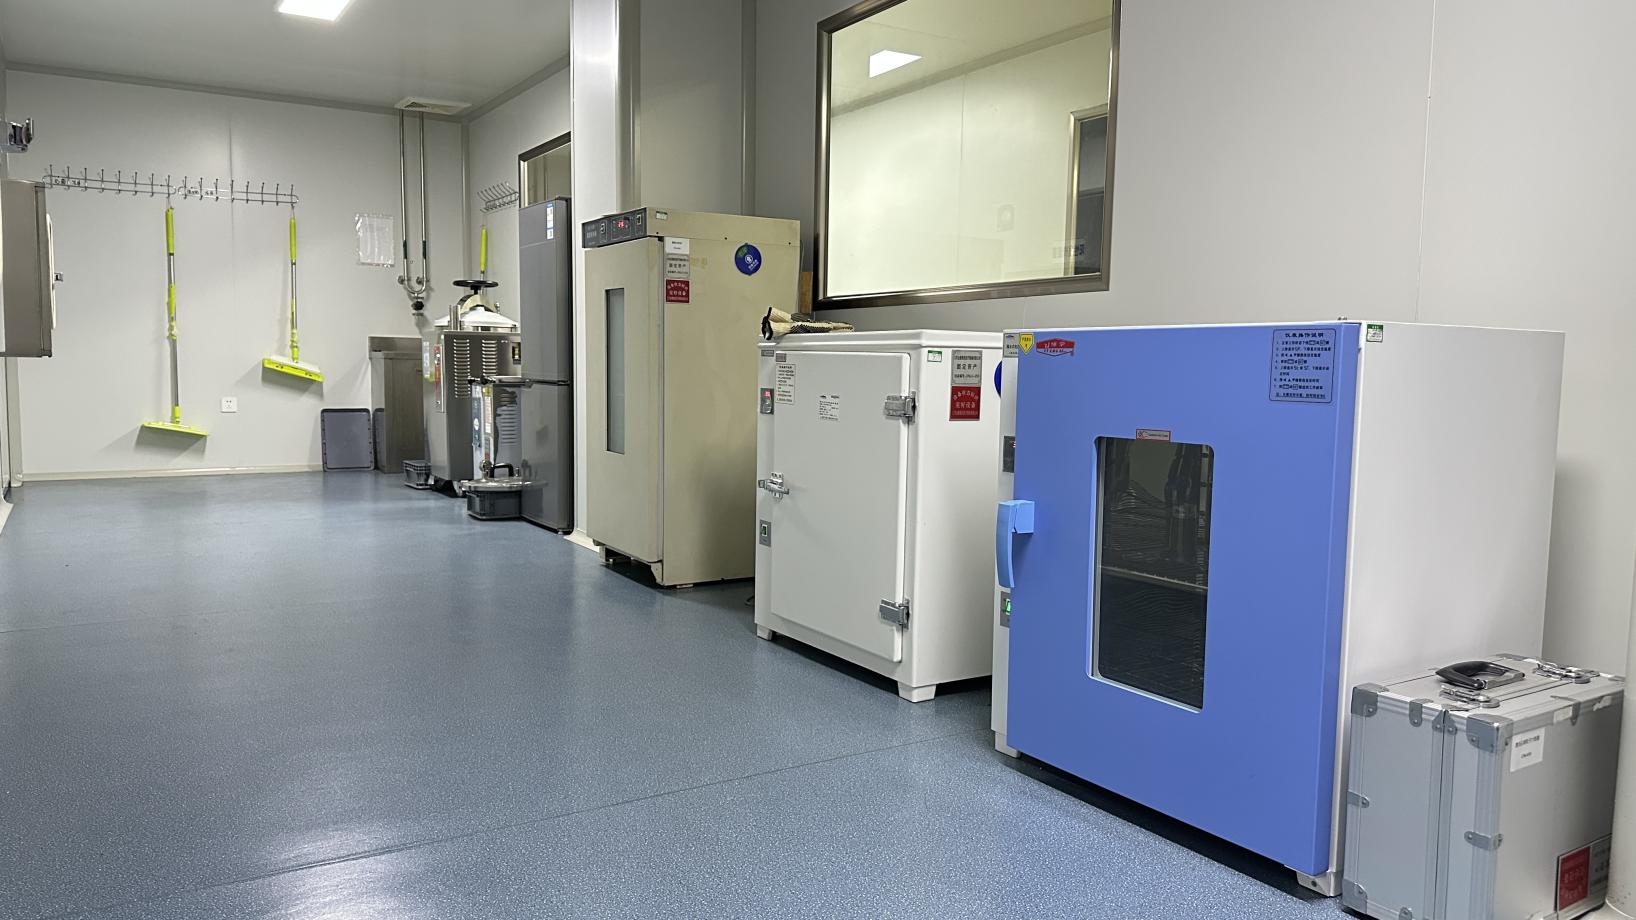
Precision Machining Center
5-Axis milling of bone saw transmission gearboxes.

Optical Projector Lab
100% dimensional inspection of cutting teeth profiles.

Mechanical Stress Testing
Evaluating blade torsional deflection and fatigue failure points.

Traceable Storage & Export
Climate-controlled finished inventory ready for global shipping.
Frequently Asked Questions from Dutch Buyers & Distributors
Clear, direct answers regarding regulatory clearance, sterilization standards, customs processing, and custom manufacturing cooperation.
Are GMV surgical saws, drills, and blades compliant with EU MDR 2017/745 requirements? +
Yes. Jiangsu GMV Medical Device Co., Ltd. operates under an audited ISO 13485:2016 medical device quality management system. Our surgical instruments and power tool families carry CE marking certifications and are supported by technical construction files, biocompatibility test records (ISO 10993 series), and sterilization validation studies compatible with EU MDR conformity declarations.
Can the surgical saw handpieces withstand Dutch CSSD steam sterilization protocols? +
Absolutely. Central Sterile Services Departments (CSSD / Centrale Sterilisatie Afdeling - CSA) in Dutch hospitals such as UMC Utrecht and Diakonessenhuis strictly follow the EN 285 standard, typically utilizing prevacuum high-pressure steam at 134°C (273°F) for 3 to 18 minutes holding time. Our power handpieces, sagittal saw attachments, chuck keys, and sterilization containment boxes are built with high-grade anodized aluminum alloys, PEEK components, and hermetically sealed drive assemblies validated specifically for repeated autoclave cycles.
What are the freight lead times and logistics routes from your factory to Utrecht? +
For urgent hospital trial batches or replacement orders, express air freight via Amsterdam Schiphol Airport (AMS) delivers within 4 to 6 business days, followed by direct customs-bonded transit to Utrecht via the A2 highway. For volume distributor shipments, maritime freight dispatches from Shanghai Port directly to the Port of Rotterdam (approx. 26–30 days transit), where our logistics partners handle EU customs release and domestic Dutch distribution.
Does GMV Medical offer OEM private label branding and customized blade hub geometries? +
Yes. As a direct custom manufacturer, we routinely engineer customized sagittal blade lengths, kerf thicknesses (from 0.4mm ultra-thin to 1.2mm rigid), and multi-vendor quick-connect hub profiles (compatible with Stryker, ConMed, Synthes, or Linvatec mounts). We provide full laser engraving for your private brand, UDI labeling, and custom sterilization tray graphic styling.
How do you guarantee material traceability and prevent counterfeit metallurgical sourcing? +
We source only certified surgical-grade alloys—predominantly Ti-6Al-4V ELI (ASTM F136 / ISO 5832-3) and implant-grade martensitic stainless steels (ASTM F899). Every raw material shipment arrives with certified mill test reports (MTR). In addition, our in-house metallurgical laboratory verifies tensile yield strength, chemical composition, and Rockwell hardness prior to CNC blanking, ensuring verifiable traceability from raw billet to finished labeled product.
Can Dutch clinical procurement teams or distributors perform on-site factory audits? +
We welcome and encourage both on-site physical audits and live video audits. Our manufacturing facility in Jinfeng Town, Suzhou, Jiangsu, China, is completely transparent to our clients. We will gladly coordinate with your quality assurance engineers or appointed European inspection bodies to walk through our CNC workshops, cleanrooms, and testing labs.
